Sincase India
online
Hi,
How can I help you ?
How can I help you ?


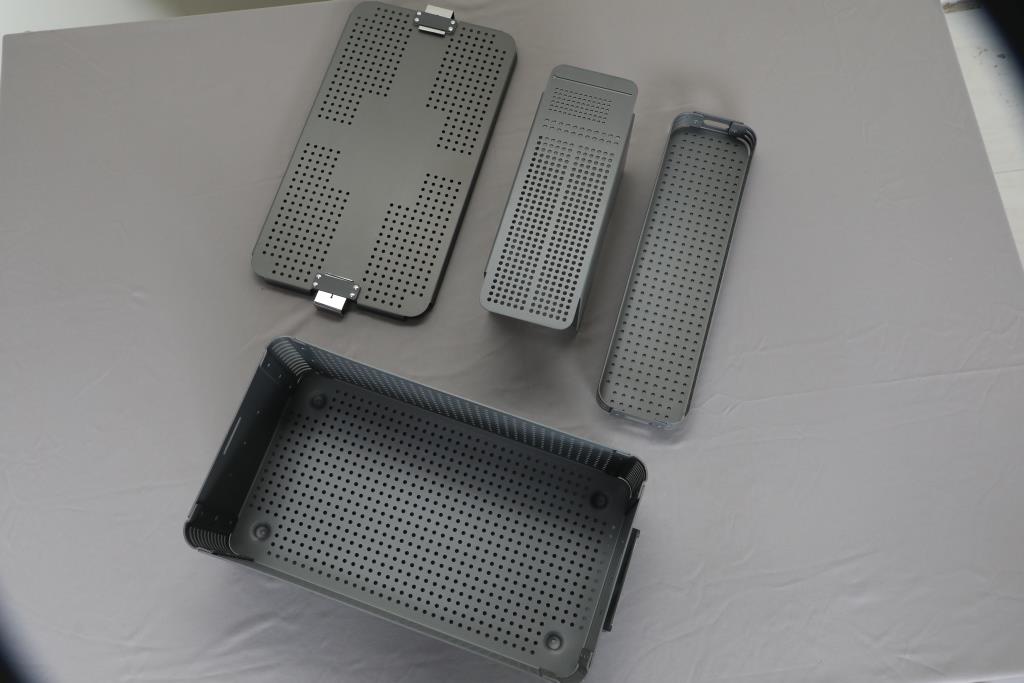
Sincase Manufacturing Pvt. Ltd. was founded in 2024 by Mr. Ranjeet Oza, founder with an innovative vision: to engineer world-class sterilizable aluminium instrument cases specifically for the healthcare industry. Recognizing that medical professionals needed storage solutions that combined superior protection, exceptional durability, and lightweight handling, we set out to manufacture products that would redefine instrument safety and organization.
As the world of healthcare continues to advance rapidly—with surgical techniques becoming more specialized and logistics demands growing more complex—we have grown alongside it. What started with a single customer has steadily expanded into a trusted network of hospitals, surgical centers, medical device manufacturers, and healthcare organizations across specialties such as general surgery, orthopedics, ophthalmology, and dental care. Day by day, more customers are choosing Sincase because they recognize the value of instrument cases engineered for real-world medical environments.
Driven by continuous innovation, strict quality control standards, and a customer-centric philosophy, we is dedicated to modernizing medical storage. By continually refining our designs and production methods, we empower healthcare professionals with intuitive, long-lasting, and dependable solutions that make daily hospital operations smoother and more reliable worldwide.
Protecting Precision. Delivering Quality.
"Our mission is to lead the evolution of medical storage with innovative, sterilizable aluminium instrument cases designed to make equipment care seamless, reliable, and effortless. Through precision design and a relentless pursuit of excellence, we empower healthcare professionals worldwide with smarter, high-performance solutions."